- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик

Which Moldbase and Standard Part Components Are Essential for Precision Injection Molds?
Precision injection molding depends on more than the cavity and core. The mold base provides the structural framework that holds the molding system together, while standard components control alignment, movement, positioning, and part ejection. If these elements are poorly matched or inaccurately manufactured, problems such as flash, uneven wear, inconsistent part dimensions, difficult mold opening, and premature tooling failure can occur. Selecting the right Moldbase and Standard Part components is therefore a fundamental step in building a reliable injection mold.
A well-engineered mold assembly combines suitable plate materials, accurate machining, dependable guiding systems, correctly selected ejector components, and compatible accessories. The required configuration varies with mold size, resin characteristics, cavity layout, injection pressure, production volume, and the specifications of the injection molding machine. Moldburger Mold Industry Co., Ltd. supplies mold bases and precision mold components for industrial applications, with published specifications covering P20 steel, 1.2311 grade steel, SUJ2 guide components, and SKD61 ejector pins. Understanding the function and selection criteria of each component helps mold designers and purchasing teams make more informed decisions.
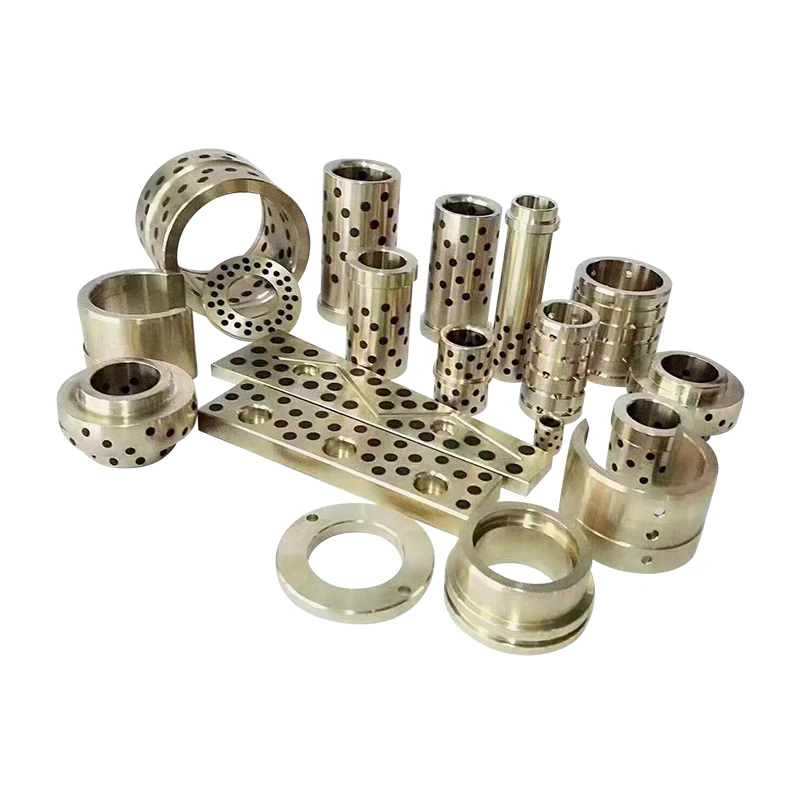
Table of Contents
1. What Mold Base Plates Are Essential for a Stable Injection Mold?
2. Which Standard Components Control Alignment, Movement, and Ejection?
3. How Should Materials, Tolerances, and Manufacturing Quality Be Evaluated?
What Mold Base Plates Are Essential for a Stable Injection Mold?
A mold base is the supporting structure that holds the cavity, core, guiding system, ejection mechanism, and other functional elements in their intended positions. During injection molding, the assembly is subjected to clamping force, injection pressure, repeated opening and closing, and thermal changes. The base must maintain dimensional stability under these operating conditions. Even when the cavity and core have been machined accurately, insufficient plate rigidity or poor alignment can affect the final molded part.
The plate arrangement depends on the mold design. A conventional two-plate mold commonly includes a top clamping plate, cavity plate, core plate, support plate, spacer blocks, ejector plates, and a bottom clamping plate. More complex tooling may require additional plates or inserts to accommodate sliders, lifters, hot runners, or special ejection arrangements. Each plate has a defined mechanical role, and its dimensions should be determined by the mold layout rather than selected only by reference to a nominal mold size.
Which plates form the main structural assembly?
The following components are commonly considered when specifying a mold base:
- Top clamping plate: Connects the stationary side of the mold to the fixed platen of the injection molding machine. It provides the mounting surface for the upper mold assembly and accommodates the sprue bushing where required.
- Cavity plate: Supports the cavity insert or contains the cavity machining directly. Its flatness, thickness, and rigidity influence how consistently the cavity side is supported during clamping.
- Core plate: Holds the core insert or core-forming features. It must maintain the designed relationship with the cavity plate throughout repeated production cycles.
- Support plate: Reinforces the core-side assembly and helps resist bending under injection pressure. The required thickness and support arrangement depend on the projected area, cavity layout, and expected molding loads.
- Spacer blocks: Create the space needed for the ejector assembly to travel. Their dimensions determine the available ejection stroke and must allow sufficient clearance for moving parts.
- Ejector retainer plate and ejector plate: Hold and drive the ejector pins, sleeves, and other ejection elements. Their movement should remain parallel and free from interference.
- Bottom clamping plate: Connects the moving side of the mold to the moving platen and provides the required mounting and support interface.
These plates work as a connected mechanical system. For example, increasing the thickness of a support plate may improve resistance to deflection, but it also affects the overall mold height and available machine space. Similarly, changing the spacer block height can influence the ejector stroke and the room available for return components. A design review should therefore consider the complete stack-up of plates, not treat every plate as an independent purchase item.
What material and hardness specifications are relevant?
Material selection should reflect the mechanical demands placed on each plate. The published ProSeries mold-base information from Moldburger Mold Industry Co., Ltd. identifies P20 pre-hardened steel and 1.2311 grade steel as base material options. The listed hardness is 28 to 32 HRC, with tensile strength of 965 to 1200 N/mm² and a minimum yield strength of 800 N/mm². These values provide a reference for evaluating the stated ProSeries configuration, but buyers should confirm the material certificate and the specification applicable to the exact order.
| Component | Published material | Published hardness | Listed surface condition |
| Clamping plates A and B | P20 / 1.2311 | 28 to 32 HRC | Ground and polished |
| Support plate S | 1045 carbon steel | 18 to 22 HRC | Ground |
| Ejector housing C and D | P20 / 1.2311 | 28 to 32 HRC | Ground |
| Guide pillars and bushings | SUJ2 bearing steel | 58 to 62 HRC | Hardened and ground |
| Ejector pins | SKD61 / H13 tool steel | 48 to 52 HRC | Precision ground |
For a general-purpose mold, P20 is frequently selected because it offers a practical balance of machinability, polishability, and mechanical performance. Higher-stress tooling may require a different steel grade or a more substantial support arrangement. The material choice should also account for the molding resin. Glass-fibre-reinforced plastics, for example, can increase abrasive wear on mold surfaces and moving components. Corrosive or moisture-sensitive processing environments may call for corrosion-resistant materials in selected areas.
How should mold-base dimensions be matched to the machine?
Physical compatibility is just as important as material quality. A mold base must fit within the machine's platen dimensions and tie-bar spacing, while its locating ring, mounting holes, overall height, and ejector interface must match the machine specification. The mold designer also needs to consider the available daylight, maximum opening stroke, minimum mold thickness, and the machine's clamping capacity.
The ProSeries published size matrix provides five reference configurations. The figures below describe the listed plate dimensions and overall height, not a universal size range for every customized mold base.
| Base size | A plate thickness | B plate thickness | S plate thickness | Overall height |
| 1515 | 50 mm | 50 mm | 25 mm | 146 mm |
| 2020 | 60 mm | 60 mm | 30 mm | 181 mm |
| 2525 | 70 mm | 70 mm | 35 mm | 216 mm |
| 3030 | 80 mm | 80 mm | 40 mm | 251 mm |
| 3535 | 90 mm | 90 mm | 45 mm | 286 mm |
When reviewing a quotation, our engineering team should receive the mold drawing, machine model, resin information, cavity arrangement, and expected production volume. These details help establish whether a standard configuration is appropriate or whether plate thickness, support positions, cooling layouts, or mounting details need modification. Moldburger Mold Industry Co., Ltd. provides mold-base options for injection molding applications, and buyers should confirm the final drawing and material schedule before production begins.
Which Standard Components Control Alignment, Movement, and Ejection?
Standard components are often smaller than the main mold plates, but their influence on repeatability is substantial. They guide the opening and closing movement, keep the mold halves in the intended relationship, release the molded product, and protect moving assemblies from unwanted displacement. A mold can have a rigid base and accurately machined cavity while still producing inconsistent parts if its guiding or ejection components are incorrectly specified.
The selection of standard components should begin with the movement and functional requirements of the mold. A simple two-plate mold may use a conventional guide pillar and bushing arrangement with ejector pins. A mold with deep ribs, cylindrical features, undercuts, or delicate cosmetic surfaces may need ejector sleeves, lifters, wear plates, or additional guiding and locking elements. The number and arrangement of these components should be determined during mold design.
Why are guide pillars and guide bushings essential?
Guide pillars and guide bushings control the relative position of the moving and stationary mold halves during opening and closing. Their purpose is to guide the assembly into the correct position before the cavity and core meet. Accurate guidance helps reduce uneven contact, protect the parting surfaces, and maintain repeatable alignment over many molding cycles.
A typical guide system includes hardened pillars installed on one side of the mold and matching bushings installed on the other. The fit between the two components must allow smooth movement while limiting excessive lateral play. A clearance that is too large can permit unwanted movement and increase the risk of misalignment. A fit that is too tight can cause friction, heat generation, scoring, or seizure, especially when lubrication is inadequate or the mold is exposed to contamination.
The published ProSeries specification identifies SUJ2 bearing steel for guide pillars and bushings, with a hardness of 58 to 62 HRC and a hardened and ground finish. This is a meaningful material and hardness reference for the listed configuration. However, buyers should also check the actual pillar diameter, working length, bushing length, fit class, surface roughness, lubrication arrangement, and dimensional tolerances on the component drawing.
Guide systems should be designed around the size and weight of the mold. Large molds may need additional guide elements or supplementary alignment features to manage uneven loading. In molds with side actions, the designer must also ensure that guide pillars, angle pins, sliders, and locking blocks do not interfere during the opening sequence. The guiding system should be inspected for wear and lubrication condition during scheduled mold maintenance.
How do ejector pins and sleeves affect part release?
The ejection system removes the molded component from the core after cooling and mold opening. Ejector pins are commonly used to push against suitable areas of the part, while ejector sleeves are useful around cylindrical bosses or core pins where a surrounding contact surface is required. The choice depends on part geometry, wall thickness, draft angle, material shrinkage, and the location of acceptable ejection marks.
Ejector pin placement is a design decision, not simply a matter of distributing pins evenly. The force should be applied to areas that can withstand the ejection load without leaving visible marks, distortion, or stress whitening. Thin walls and narrow ribs may require a different ejection arrangement from thick structural sections. If the part grips the core strongly, the designer may need to increase the effective ejection area or revise the draft and surface finish rather than rely on a few heavily loaded pins.
Ejector pins must be straight, correctly fitted, and sufficiently supported. Excessive unsupported length can increase the risk of bending. Incorrect pin height can create witness marks or uneven release, while poor alignment may cause the pin to rub against its hole. Ejector sleeves require similar attention to concentricity and running clearance because they operate around a core pin and may be exposed to side loads during ejection.
For the published ProSeries configuration, the listed ejector pin material is SKD61 H13 tool steel, with a hardness of 48 to 52 HRC and a precision-ground finish. This specification should be treated as a reference for the stated product configuration rather than an assumption that every ejector pin or sleeve uses the same grade. Buyers should confirm the diameter, length, head style, tip geometry, hardness, and any special coating or surface treatment required for the application.
Which other components complete the mold movement system?
Several additional components may be required to achieve reliable mold operation. Their use depends on the mold architecture and the type of molded product.
- Return pins: Help return the ejector assembly to its original position as the mold closes. Their length and contact arrangement must suit the ejector plate design.
- Springs: Provide return force or controlled movement in selected mechanisms. Spring selection should consider working load, compression range, fatigue life, operating temperature, and available installation space.
- Locating ring: Positions the mold relative to the injection machine nozzle and locating opening. Its dimensions must match the machine interface and the mold's sprue arrangement.
- Sprue bushing: Provides the entry path for molten plastic from the machine nozzle into the mold runner system. Nozzle radius, orifice dimensions, and seating geometry need to be compatible.
- Wear plates: Protect sliding contact surfaces in areas such as sliders and other moving mold mechanisms. They can be replaced when wear reaches an unacceptable level, helping protect more expensive mold structures.
- Guide accessories: May include additional guides, stops, and alignment components for specific mold layouts. The exact configuration should follow the approved mold drawing.
- Locks and limit components: Control selected stages of mold movement or provide positioning functions in designs that require them.
- Seals and plugs: Support cooling channel and fluid circuit requirements where specified by the mold design. Their material and pressure rating must be suitable for the operating conditions.
Not every mold requires every component in this list. For example, a basic mold may not need lifters or complex locking blocks, while a mold with side undercuts may depend on sliders, angle pins, and wear plates to complete its movement sequence. The component list should be generated from the mold assembly drawing and bill of materials, with each part assigned a clear function and reference number.
Moldburger Mold Industry Co., Ltd. lists guide pillars and wear plates, guides and other mold accessories, and ejector pins and ejector sleeves among its mold component categories. When sourcing these parts, our purchasing specification should identify the component type, drawing number, material, hardness, dimensions, surface treatment, and quantity. This reduces ambiguity between visually similar components that may have different functional requirements.
How Should Materials, Tolerances, and Manufacturing Quality Be Evaluated?
Precision is not established by a material name or a machine list alone. It is the result of a controlled relationship between design requirements, raw material condition, machining processes, heat treatment, grinding, assembly, and inspection. A component may meet its nominal dimensions but still perform poorly if its flatness, parallelism, concentricity, hardness, or surface finish is unsuitable for the application. Buyers should therefore evaluate the manufacturing and inspection requirements alongside the product specification.
How should steel grades be matched to component functions?
Different mold components experience different forms of mechanical stress and wear. A large plate must provide structural support and maintain its geometry. A guide pillar experiences repeated sliding contact. An ejector pin is exposed to compressive force, friction, and repeated movement. Selecting one material for every component would ignore these different operating conditions.
The product information published by Moldburger Mold Industry Co., Ltd. identifies several steel options for mold-base applications, including P20, 4140, H13, stainless steel, and S7. The listed descriptions associate P20 with general-purpose mold applications and good machinability, 4140 with strength and toughness, H13 with heat resistance, stainless steel with corrosion resistance, and S7 with impact resistance. These are selection references, not interchangeable guarantees. The correct grade depends on the component, resin, processing temperature, expected wear, and maintenance requirements.
For example, P20 may be suitable for many general-purpose plates, while H13 is often considered where higher thermal demands or specific wear conditions justify its use. A stainless grade may be relevant in applications where corrosion resistance is important, but the exact grade and heat treatment still need confirmation. The buyer should also distinguish between the base material of the plate and the materials used for inserts, guide elements, ejectors, and wear components.
Heat treatment is another important consideration. Hardness affects resistance to indentation and wear, but hardness alone does not describe toughness, dimensional stability, or resistance to cracking. If a component is hardened after rough machining, the manufacturing plan should account for possible distortion and the need for finish grinding. For components requiring close fits, inspection should take place after the final machining and heat treatment stages, not only before them.
Which dimensional tolerances deserve the closest attention?
Not every dimension on a mold drawing has the same functional importance. A plate's overall length and width may have a relatively broad tolerance, while guide holes, locating features, insert pockets, and sliding interfaces may require much closer control. A useful inspection plan identifies the critical-to-function dimensions and defines how they will be measured.
Typical areas requiring attention include:
- Plate flatness and parallelism: Influence how the mold closes and how clamping loads are distributed across the assembly.
- Guide hole position: Determines the relationship between the guide system and the cavity and core plates.
- Guide pillar diameter and straightness: Affect running fit, friction, and repeatable alignment.
- Insert pocket dimensions: Determine whether cavity and core inserts can be located and retained correctly.
- Ejector hole position and diameter: Affect pin movement and the risk of rubbing or seizure.
- Parting surface condition: Influences mold closure and the risk of flash caused by poor contact or damage.
- Mounting and locating features: Must match the injection machine and the approved mold design.
The ProSeries mold-base page lists CNC machining for plates and components and describes the manufacturing approach as intended to achieve accurate alignment and fit. A separate mold-making specification page lists a standard size range from 150 mm by 150 mm to 600 mm by 600 mm, a standard surface finish of Ra 0.4 micrometres, and a tolerance of plus or minus 0.01 mm on critical dimensions. These figures belong to that published specification and should not be automatically applied to every mold-base series or individual component.
Another injection mold base page lists a different set of standard sizes, surface finish information, and model series. Because published product pages may describe different configurations, buyers should request one consolidated drawing and specification sheet for the selected model. The final quotation should state which tolerance applies to each critical dimension, how surface roughness is measured, and whether inspection records are supplied with the order.
What manufacturing and inspection processes support repeatability?
Machining capability is relevant only when it is connected to the dimensions and features required by the mold design. CNC milling and drilling are used to produce plate profiles, holes, pockets, and mounting features. Precision grinding can improve flatness, parallelism, and surface condition. Wire EDM may be used for profiles or features that are difficult to produce by conventional cutting. Heat treatment may be required to achieve specified hardness, while dimensional inspection verifies whether the finished part conforms to the drawing.
The company profile of Moldburger Mold Industry Co., Ltd. lists CNC machines from Makino, Dawei, and FANUC, electrical discharge machines from Makino and Sodick, slow wire-feeding machines, Okamoto grinders, lathes, and Hexagon coordinate measuring equipment. It also reports a team of 30 design engineers and more than 100 professional and technical personnel. These published resources indicate the range of equipment and personnel described by the company, while the process used for an individual order should be confirmed against its actual manufacturing plan.
A coordinate measuring machine can be used to inspect geometric features and compare measured positions with the engineering drawing. For simpler dimensions, calibrated gauges, micrometers, bore gauges, height gauges, and surface roughness instruments may be appropriate. The inspection method should be selected according to the tolerance and geometry being checked. A measurement result is only meaningful when the instrument has suitable resolution, calibration status, and a defined measurement procedure.
Quality documentation should ideally include a material certificate, hardness report where specified, dimensional inspection results for critical features, and records of any special process required by the drawing. For repeated orders, retaining approved drawings and inspection criteria helps maintain consistency between batches. If a component is intended to replace an existing part, the buyer should provide the original drawing or a verified sample and identify any changes from the previous revision.
How can buyers reduce sourcing and assembly risks?
Procurement teams often compare mold components by unit price and delivery time. Those factors matter, but they should be assessed against compatibility, inspection requirements, and the cost of production interruption. A low-cost guide component that wears prematurely can lead to alignment problems, maintenance work, and rejected molded parts. A correctly specified component may have a higher purchase price but offer better lifecycle value if it reduces downtime and replacement frequency.
Before placing an order, use the following technical review points:
- Confirm the mold type, plate arrangement, and machine interface.
- Provide the latest approved mold assembly drawing and component drawings.
- Identify material grades, hardness requirements, and heat treatment conditions.
- Specify critical dimensions, geometric tolerances, and surface roughness.
- Confirm whether the components must follow DME, HASCO, FUTABA, or another nominated standard.
- Check interchangeability with existing mold parts and the intended replacement components.
- Agree on inspection documents, packaging, identification, and traceability requirements.
- Review the delivery schedule in relation to machining, heat treatment, grinding, and final inspection.
The injection mold base information published by the supplier references DME, HASCO, and FUTABA compatibility. Buyers should still identify the specific standard series and dimensions required. The phrase "international standard" is not sufficient by itself because different systems may use different dimensions, fits, and component conventions. Our technical purchasing documents should specify the standard, part number, and revision wherever interchangeability is required.
For custom projects, Moldburger Mold Industry Co., Ltd. can be evaluated on its ability to review drawings, manufacture the required plate and component configuration, and provide relevant quality information. Our factory coordination should focus on resolving technical questions before production, particularly where the order includes non-standard dimensions or replacement components. A clear approval process helps prevent avoidable revisions after machining has started.
Conclusion
A precision injection mold relies on a stable mold base and a coordinated set of standard components. Clamping plates, cavity and core plates, support plates, spacer blocks, and ejector housings provide the structural foundation. Guide pillars, bushings, ejector pins, sleeves, return pins, locating rings, sprue bushings, and wear components support accurate movement and reliable part release. Material selection, dimensional control, machine compatibility, and inspection records determine whether these components work together as intended.
Moldburger Mold Industry Co., Ltd. offers mold-base and standard-component solutions supported by published material specifications, machining resources, and inspection equipment. If you are developing a new injection mold or sourcing replacement components, send our team your drawings, material requirements, machine details, and expected production conditions. Request a technical review and quotation to identify a suitable configuration for your tooling project.
Frequently Asked Questions
Q: What is the difference between a mold base and standard mold components?
A: A mold base is the structural assembly of plates and supporting elements that holds the cavity, core, guiding system, and ejection mechanism. Standard mold components are the functional parts installed within or around that assembly, such as guide pillars, guide bushings, ejector pins, ejector sleeves, return pins, locating rings, and sprue bushings. The mold base provides structural support, while standard components control alignment, movement, positioning, and part release. Both must be specified together to achieve reliable mold operation.
Q: Which steel is commonly used for precision injection mold bases?
A: P20 and 1.2311 pre-hardened steel are commonly used for general-purpose mold-base plates because they offer a practical combination of machinability and mechanical performance. Other grades may be selected according to the application. For example, 4140 is associated with strength and toughness, H13 with heat resistance, stainless steel with corrosion resistance, and S7 with impact resistance. The final choice should consider the mold structure, resin, operating temperature, wear conditions, required hardness, and the supplier's material documentation.
Q: Why are guide pillars and bushings important in injection mold accuracy?
A: Guide pillars and bushings control the relative position of the two mold halves as the mold opens and closes. Correctly matched components help the cavity and core meet in the intended position, reducing unwanted movement and protecting the parting surfaces. Their diameter, straightness, fit, hardness, surface finish, and lubrication requirements all influence performance. Excessive clearance can contribute to misalignment, while an overly tight fit can cause friction, scoring, or seizure during repeated operation.
Q: How should ejector pins be selected for a plastic injection mold?
A: Ejector pins should be selected according to the molded part's geometry, wall thickness, material shrinkage, draft, and expected ejection resistance. Their contact positions should distribute the release force without causing visible marks or part distortion. Pin diameter, length, head style, tip geometry, hardness, and fit within the ejector plate should be checked against the mold drawing. Ejector sleeves may be more suitable around cylindrical bosses or core pins where a surrounding contact surface is needed.
Q: What information should buyers provide when ordering a customized mold base?
A: Buyers should provide the latest mold assembly drawing, plate dimensions, machine model, tie-bar spacing, platen details, locating ring and mounting requirements, ejector interface, cavity arrangement, resin type, and expected production conditions. The order should also specify material grades, hardness, critical tolerances, surface finish, applicable standards, and required inspection documents. Providing this information before quotation helps the manufacturer assess compatibility, identify special machining requirements, and reduce the risk of dimensional or assembly problems.